When purchasing copper busbars, terminals, or contacts, first explain where the part will be used, which areas carry current, and where wires will be connected. Then discuss tarnish and corrosion requirements. On the same part, an appearance surface that should retain its copper color and a mating surface that forms an electrical joint may need different treatments.
1. Define what needs protection before naming a treatment
Tarnish resistance, corrosion resistance, electrical contact, and solder wettability are different requirements. A change in copper color does not necessarily mean that the part has lost its function. A bright surface does not prove that joint resistance meets the requirement. List appearance criteria and functional checks separately in the RFQ.
For example, an indoor decorative copper part may mainly need to arrive without fingerprints or obvious discoloration. A terminal soldered after storage needs to wet under the specified soldering process. A bolted mating surface carrying current needs to perform as an assembled joint. A single “anti-oxidation” note cannot define all three requirements.
Start the RFQ with the following information. Items that are not yet decided can be marked “to be discussed”:
- Copper grade, temper, sheet thickness, and drawing revision; whether alternative materials require approval.
- Indoor, outdoor, or specific corrosive exposure, together with the intended storage and assembly arrangements.
- Surfaces whose appearance matters, and the locations of electrical contacts, crimps, and solder joints.
- An existing treatment specification, approved sample, or desired appearance; if no treatment has been chosen, describe the application.
- Required inspections, records, packaging, and compliance documents, including whether they are part of the quotation.
Use the stamped copper busbar and terminal RFQ guide to prepare material, hole-location, and assembly information. This article focuses on surface treatment and acceptance notes.
2. Distinguish passivation, anti-tarnish treatment, sealing, and electroplating
“Copper passivation” in a purchasing document may refer to different treatment systems. The term alone does not define film composition, thickness, or performance in subsequent assembly. Anti-tarnish describes an objective; sealing adds a protective layer; electroplating deposits another metal on the copper substrate. State the process type and coverage rather than relying on a name.
Some organic anti-oxidation films bond to the copper surface and slow surface reactions. Other protection systems use an overlying coating. Their effects on subsequent soldering and electrical contact need to be confirmed separately.[1][2]
| Wording in the RFQ | What must be clarified | What the name alone cannot establish |
|---|---|---|
| Copper passivation or anti-tarnish treatment | Treatment system, coverage, appearance target, and whether the part will later be soldered or used for electrical contact | A fixed film thickness, storage life, or salt-spray result |
| Sealing after treatment | Type of sealant, application areas, whether contact surfaces may be covered, and whether removal is required | That every sealant improves protection, or that every sealant is suitable for electrical-contact surfaces |
| Tin, nickel, silver, or other electroplating | Plating specification, thickness range, underlayer requirements, selective-treatment boundaries, and dimensions after treatment | That a metal finish automatically provides acceptable electrical-contact and soldering performance |
| Leave copper bare | Areas receiving no additional treatment, protection during storage and transport, and preparation before assembly | That bare copper will indefinitely retain its original color and surface condition |
If sealing is proposed, compare the results of the complete treatment system on actual parts. Film continuity, pretreatment, and subsequent use all affect the assessment; adding a sealing step does not by itself demonstrate improved performance.[2] Provide any prohibited-substance requirements or specific compliance documents with the RFQ, so that the supplier does not quote a different system first.
3. Use functional areas to define which surfaces may be treated
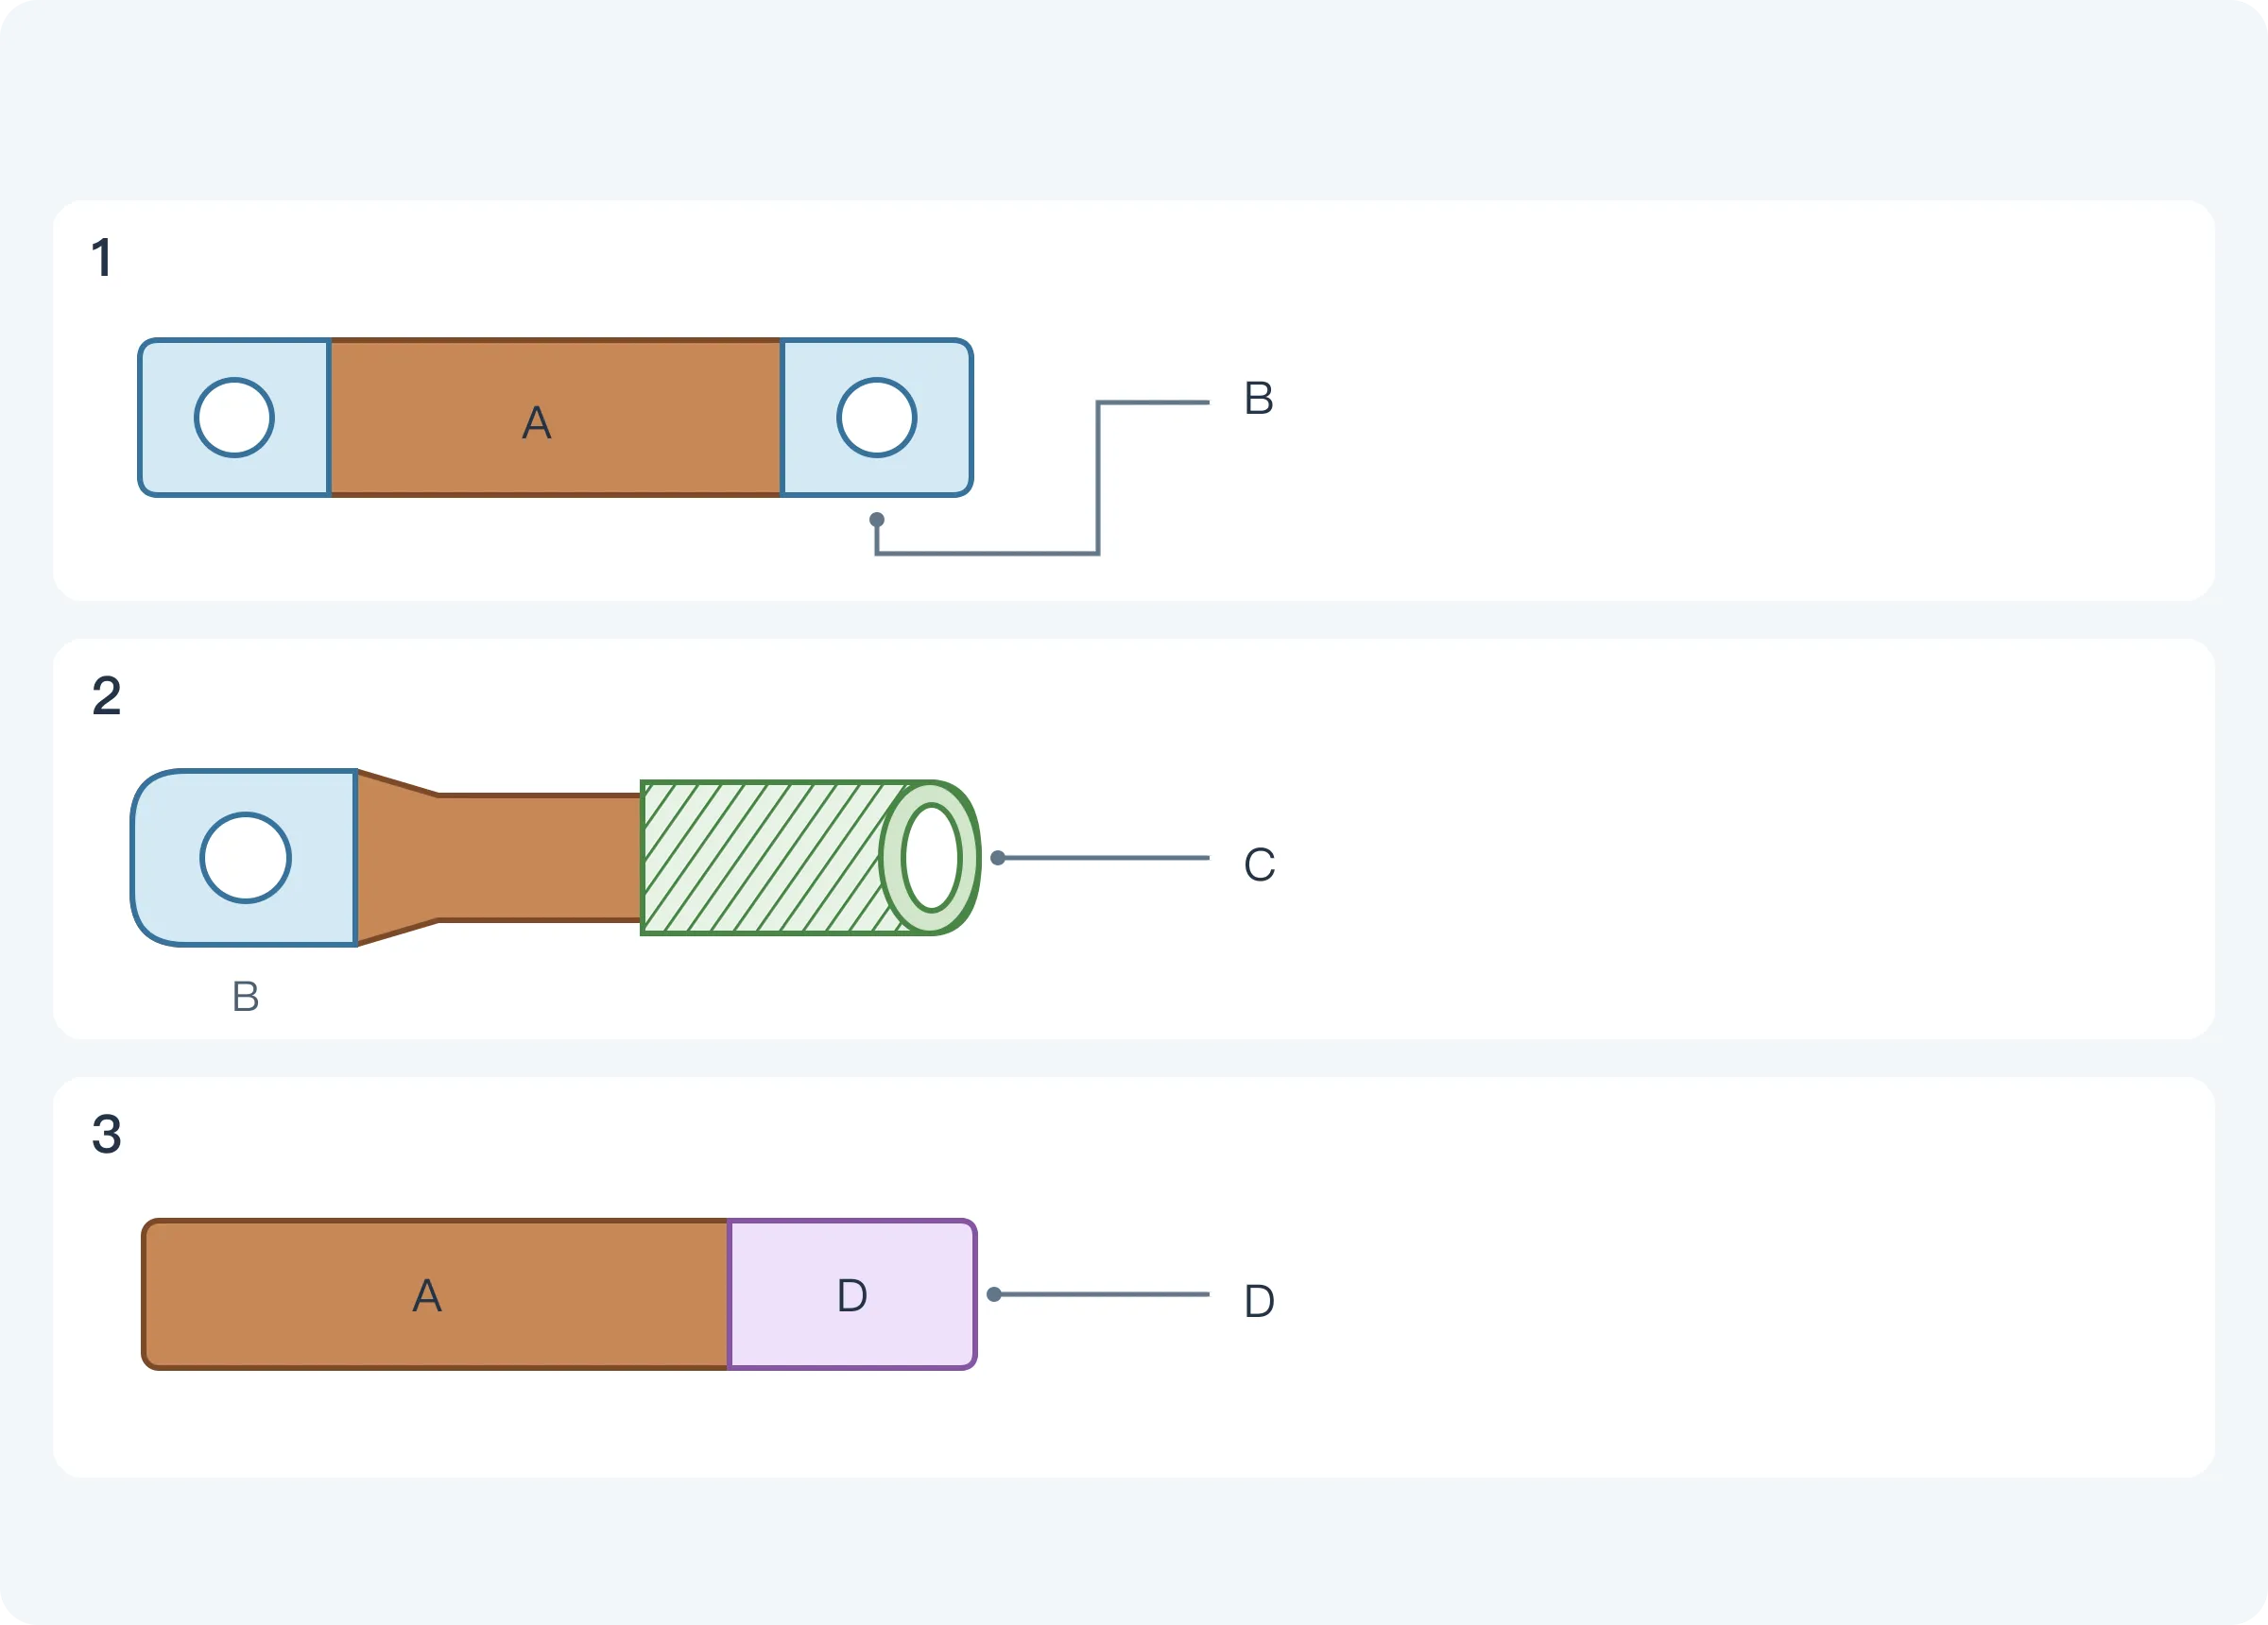
Mark the functional areas before deciding how to treat each one. A bolted contact surface is usually the face that overlaps another conductor, rather than just the hole wall. The crimping area concerns the internal surface touching the wire. The soldering area concerns the surface that solder must wet. Show both sides and local boundaries on the drawing so that the supplier does not treat only the visible side.
| Area | How the customer can describe its use | What the quotation and drawing should specify |
|---|---|---|
| A — Appearance area | “This section needs a uniform copper color at delivery” | Appearance reference, acceptable color variation, treatment route, and protective packaging |
| B — Bolted contact area | “This face will be clamped against another copper busbar to carry current” | Actual overlap boundary, mating material, permitted films or plating, assembly conditions, and joint-inspection requirements |
| C — Crimping area | “This section wraps around the wire to form a crimped connection” | Extent of the internal surface touching the wire, terminal and wire combination, and checks after crimping |
| D — Soldering area | “Solder needs to wet this area” | Soldering materials and process, storage conditions, compatibility of the surface treatment, and solder-wettability checks |
Area B can be specified to exclude a particular sealant film, or selective electroplating or another approved approach can be evaluated. The key is to define the permitted surface condition. Selective-treatment boundaries, masking locations, and critical mating dimensions after treatment should also be traceable on the drawing. Do not turn “leave every contact surface bare” or “nickel-plate every soldering surface” into a universal rule.
4. Check electrical joints and solder wettability under the relevant assembly conditions
A continuous insulating film over an actual electrical-contact location may obstruct metal-to-metal contact. Joint resistance also depends on surface condition, contact pressure, and connection design, however. It is therefore inaccurate to say that every material called a “sealant” necessarily increases contact resistance. Some approved contact compounds fill voids in the contact area and slow corrosion; their purpose differs from that of an appearance-protection film.[2]
For a bolted connection, the RFQ can ask the supplier to check the joint using specified mating parts, tightening conditions, and measurement locations. Attach the relevant specification if the project sets resistance or temperature-rise limits. “Electrical continuity” alone does not define long-term service requirements, and a milliohm value from a different terminal should not become a universal threshold.
Films on soldering surfaces also need to be distinguished by their purpose. Some organic films designed to preserve copper solderability can be removed by compatible flux and soldering temperatures, allowing solder to contact the copper. Both the film's protection against oxidation during storage and its removal during soldering affect wetting. An organic film does not necessarily obstruct soldering, and an appearance sealant is not automatically a solderability-preservation film.[1]
When preparing actual samples, arrange separate checks:
- Check appearance areas under consistent viewing conditions against an approved sample.
- Check bolted joints using the project's assembly and electrical-inspection methods.
- Check crimping areas against the acceptance requirements for the terminal, wire, and crimping process.
- Check soldering areas using the actual storage condition, solder, flux, and soldering process.
These checks answer different questions. A record of acceptable surface condition after salt spray cannot replace verification of electrical joints, crimps, or solder wettability.
5. Specify salt-spray hours together with the test method and acceptance criteria
“96 hours of neutral salt spray” is an exposure condition that can be agreed for a project, not a default acceptance threshold for copper passivation. ISO 9227 includes neutral salt spray (NSS), acetic acid salt spray (AASS), and copper-accelerated acetic acid salt spray (CASS). These methods are not interchangeable merely because their durations match. Neither ISO 9227 nor ASTM B117 defines the specimens, exposure duration, or acceptance criteria for a specific product.[3][4]
A copper-part note should say more than “no red rust.” Describe discoloration, corrosion products, and pitting on the copper according to the project requirements. If the specimen also includes steel bolts, define the hardware's evaluation scope separately. A single criterion for the copper body and steel hardware can obscure what is being assessed.
| Required item | What needs to be specified |
|---|---|
| Method and edition | A defined method and its adopted edition; for ISO 9227, state NSS, AASS, or CASS |
| Exposure duration | The duration agreed for this project, for example 96 hours |
| Specimens | Actual parts or test coupons, quantity, material grade, treatment batch, and whether tested individually or as an assembly |
| Exposure scope | Whether masked areas, hole edges, cut edges, and hardware are assessed, and how the specimen mounting arrangement is confirmed |
| Evaluation procedure | Cleaning, drying, and observation timing after removal, plus lighting, photographs, and record requirements |
| Acceptance criteria | Permitted discoloration; prohibited corrosion products, pitting, or film damage; whether functional checks are also required |
| Report and cost | Who performs the test, whether it is included in the quotation, and which specimens and batches the report must identify |
One use of salt-spray testing is to assess the consistency of the same treatment route using the same method. An isolated salt-spray result cannot be converted directly into years of outdoor use, and it is unsuitable for assigning a universal corrosion-resistance ranking to different materials.[3][4] Chloride exposure, humidity, sulfur-containing atmospheres, and actual assembled joints may require different verification arrangements.
6. A completed example of a salt-spray acceptance note
The example below uses the copper busbar areas in Figure 1 to show how to specify the conditions fully. It defines a surface-appearance and corrosion check; all values and acceptance criteria are illustrative. Before testing, the buyer and laboratory should confirm that project arrangements such as post-test treatment and observation timing are compatible with the referenced method, then include them in the approved quality plan.
| Item | Example entry |
|---|---|
| Part identification | CP-01, Rev A; material C11000, H02 temper, 2.0 mm thick |
| Treatment coverage | Area A uses the anti-tarnish treatment plus sealant system approved on the sample; area B remains bare copper, with neither that anti-tarnish film nor that sealant film applied |
| Approval and changes | Sample-approval record CP-01-F1; retain records of the treatment system and functional areas, and reconfirm after any change to the system or coverage |
| Method | ISO 9227:2022, NSS, together with Amd 1:2024; the laboratory follows the applicable documents |
| Exposure duration and specimens | 96 hours; 3 actual parts from the same treatment batch, tested individually without mating busbars or bolts; no additional scribe |
| Exposure and mounting | Expose both areas A and B; include hole edges and cut edges in the observations. Support contact points are used only for mounting, marked and photographed beforehand, and excluded from appearance evaluation. The laboratory records a compliant mounting arrangement |
| Post-test treatment | Handle residual salt in accordance with the referenced method. Do not polish, brush, or use cleaning agents to remove corrosion products. Evaluate and photograph after drying indoors for 24 hours |
| Observation method | Use normal or corrected vision at approximately 30 cm under the same diffuse lighting. Record close-up photographs of both faces, hole edges, and cut edges, and compare them with the pre-test photographs |
| Acceptance criteria | Neither area A nor area B may have visually observable pitting or powdery corrosion products. Uniform darkening is permitted; visually distinguishable localized discoloration is not. The sealant film in area A may not show visible blistering or peeling. All 3 specimens must comply |
| Functional scope | This check assesses surface condition only. Electrical contact in assembled area B is verified separately under the product's electrical-inspection specification; this check does not replace that verification |
| Report and quotation | Quote the test cost separately. The report lists the part revision, material grade, treatment batch, specimen IDs, method and edition, actual exposure duration, mounting, post-test treatment, photographs, and conclusions for each specimen |
The 3 specimens, 24 hours, 30 cm, and appearance criteria here are project conditions chosen to illustrate a complete note, rather than quantities or thresholds automatically specified by a salt-spray standard. The example record IDs simply show how drawings, treatment records, and samples can be linked.
This note permits uniform darkening but rejects pitting and the specified film damage. If the customer's actual objective is to retain the approved sample's copper color after testing, define separate color criteria and a reference. Do not test under permissive criteria and then describe the result as showing no color change.
7. Cleaning, handling, and packaging also affect the delivered condition
The selected process needs to remove oil and surface contamination before treatment and control recontamination. After treatment, protect the surface against fingerprints, scratches, and damp packaging. Fingerprints may cause uneven copper discoloration, but that does not establish that a single bare-hand touch defeats every protective film.[1][2]
State in the RFQ whether parts will be stored for extended periods between stamping, surface treatment, and assembly. Choose packaging for the application: partitioned trays, bag materials, or anti-tarnish materials used to protect appearance must also be compatible with contact surfaces and subsequent soldering. “Use anti-tarnish packaging” alone does not define the material, storage conditions, or storage period.
At receiving inspection, first check the drawing revision, batch, treatment boundaries of the functional areas, and packaging condition. Then sample the parts for the agreed appearance and functional checks. If discoloration is found, retain the original packaging, batch details, and photographs to help distinguish treatment, storage, and handling problems.
8. Define treatment, inspection, and quotation scope in the same RFQ
Two quotations should refer to the same drawing, treatment coverage, and acceptance conditions. If one includes selective masking, approved samples, and test reports while the other covers only whole-part anti-tarnish treatment, the price difference cannot be interpreted simply as a difference in manufacturing cost.
The quotation can list part manufacture, surface treatment, selective masking, samples and testing, reports, and packaging separately. See the metal-part surface-finish RFQ guide for more detail on specifying plating coverage and inspection costs.
Even if the process has not been chosen, you can send a drawing, sketch, or photograph. Mark the areas that carry current, connect to wires, or require soldering, and explain the service environment, expected quantity, and current questions. Discuss surface-treatment options around this information, then record the agreed requirements in the drawing and quotation. When the information is ready, send your copper-part RFQ.
- [1] N. R. Sorensen and F. M. Hosking — Solderability preservation through the use of organic inhibitors, Sandia National Laboratories, SAND-94-2749C (1994)
- [2] David Chapman and Toby Norris — Copper for Busbars: Guidance for Design and Installation, CDA/ECI (2014), pp. 94 and 101–104
- [3] ISO 9227:2022 — Corrosion tests in artificial atmospheres: Salt spray tests
- [4] ASTM B117-26a — Standard Practice for Operating Salt Spray (Fog) Apparatus