Metal Stamping Tooling and Die Making
HARVLAND develops stamping dies around the required metal part, from process planning and die design through component manufacture, assembly and trial correction. The confirmed drawing and sample requirements guide the work through to production release.
Turn the part drawing into a workable die structure
Die development starts with the operations needed to make the part. Geometry, material and production volume guide the choice of tooling, station sequence and locating method.
- Review cutting, bending and drawing operations against the part requirements.
- Define punches, die sections, support, guidance and stripping as a working assembly.
- Allow access for assembly, adjustment and replacement of wear components.
Make and fit the components that control the part
Plates, working inserts and locating components are made to the confirmed die design and fitted into the assembly. Component fit and coordinated movement are checked before trial stamping.
- Check working clearances, alignment and support at the relevant features.
- Check opening, closing, stripping and scrap-clearance paths.
- Record adjustments that affect the die setup or later maintenance.
Use stamped samples to guide tool correction
Trials reveal how the material behaves in the assembled die. Measured parts guide adjustments to dimensions, springback, burrs and surface marks.
- Compare samples with the drawing revision and agreed inspection points.
- Record deviations, tool changes and repeat sample checks.
- Plan the required trial rounds and sample quantities for the project.
Confirm the sample, then define how the die will be used
Sample approval, pilot production and tooling handover have different purposes. Confirm the applicable release steps and the records that support each one.
- Agree dimensional, appearance and mating checks before approval.
- Define ownership, storage, maintenance and repair responsibilities.
- If tool handover is required, agree press compatibility and the drawings, spares and documents included.
Progressive die drawings
Explore the support-bracket progressive die drawing and enlarge the views to see the structural details.
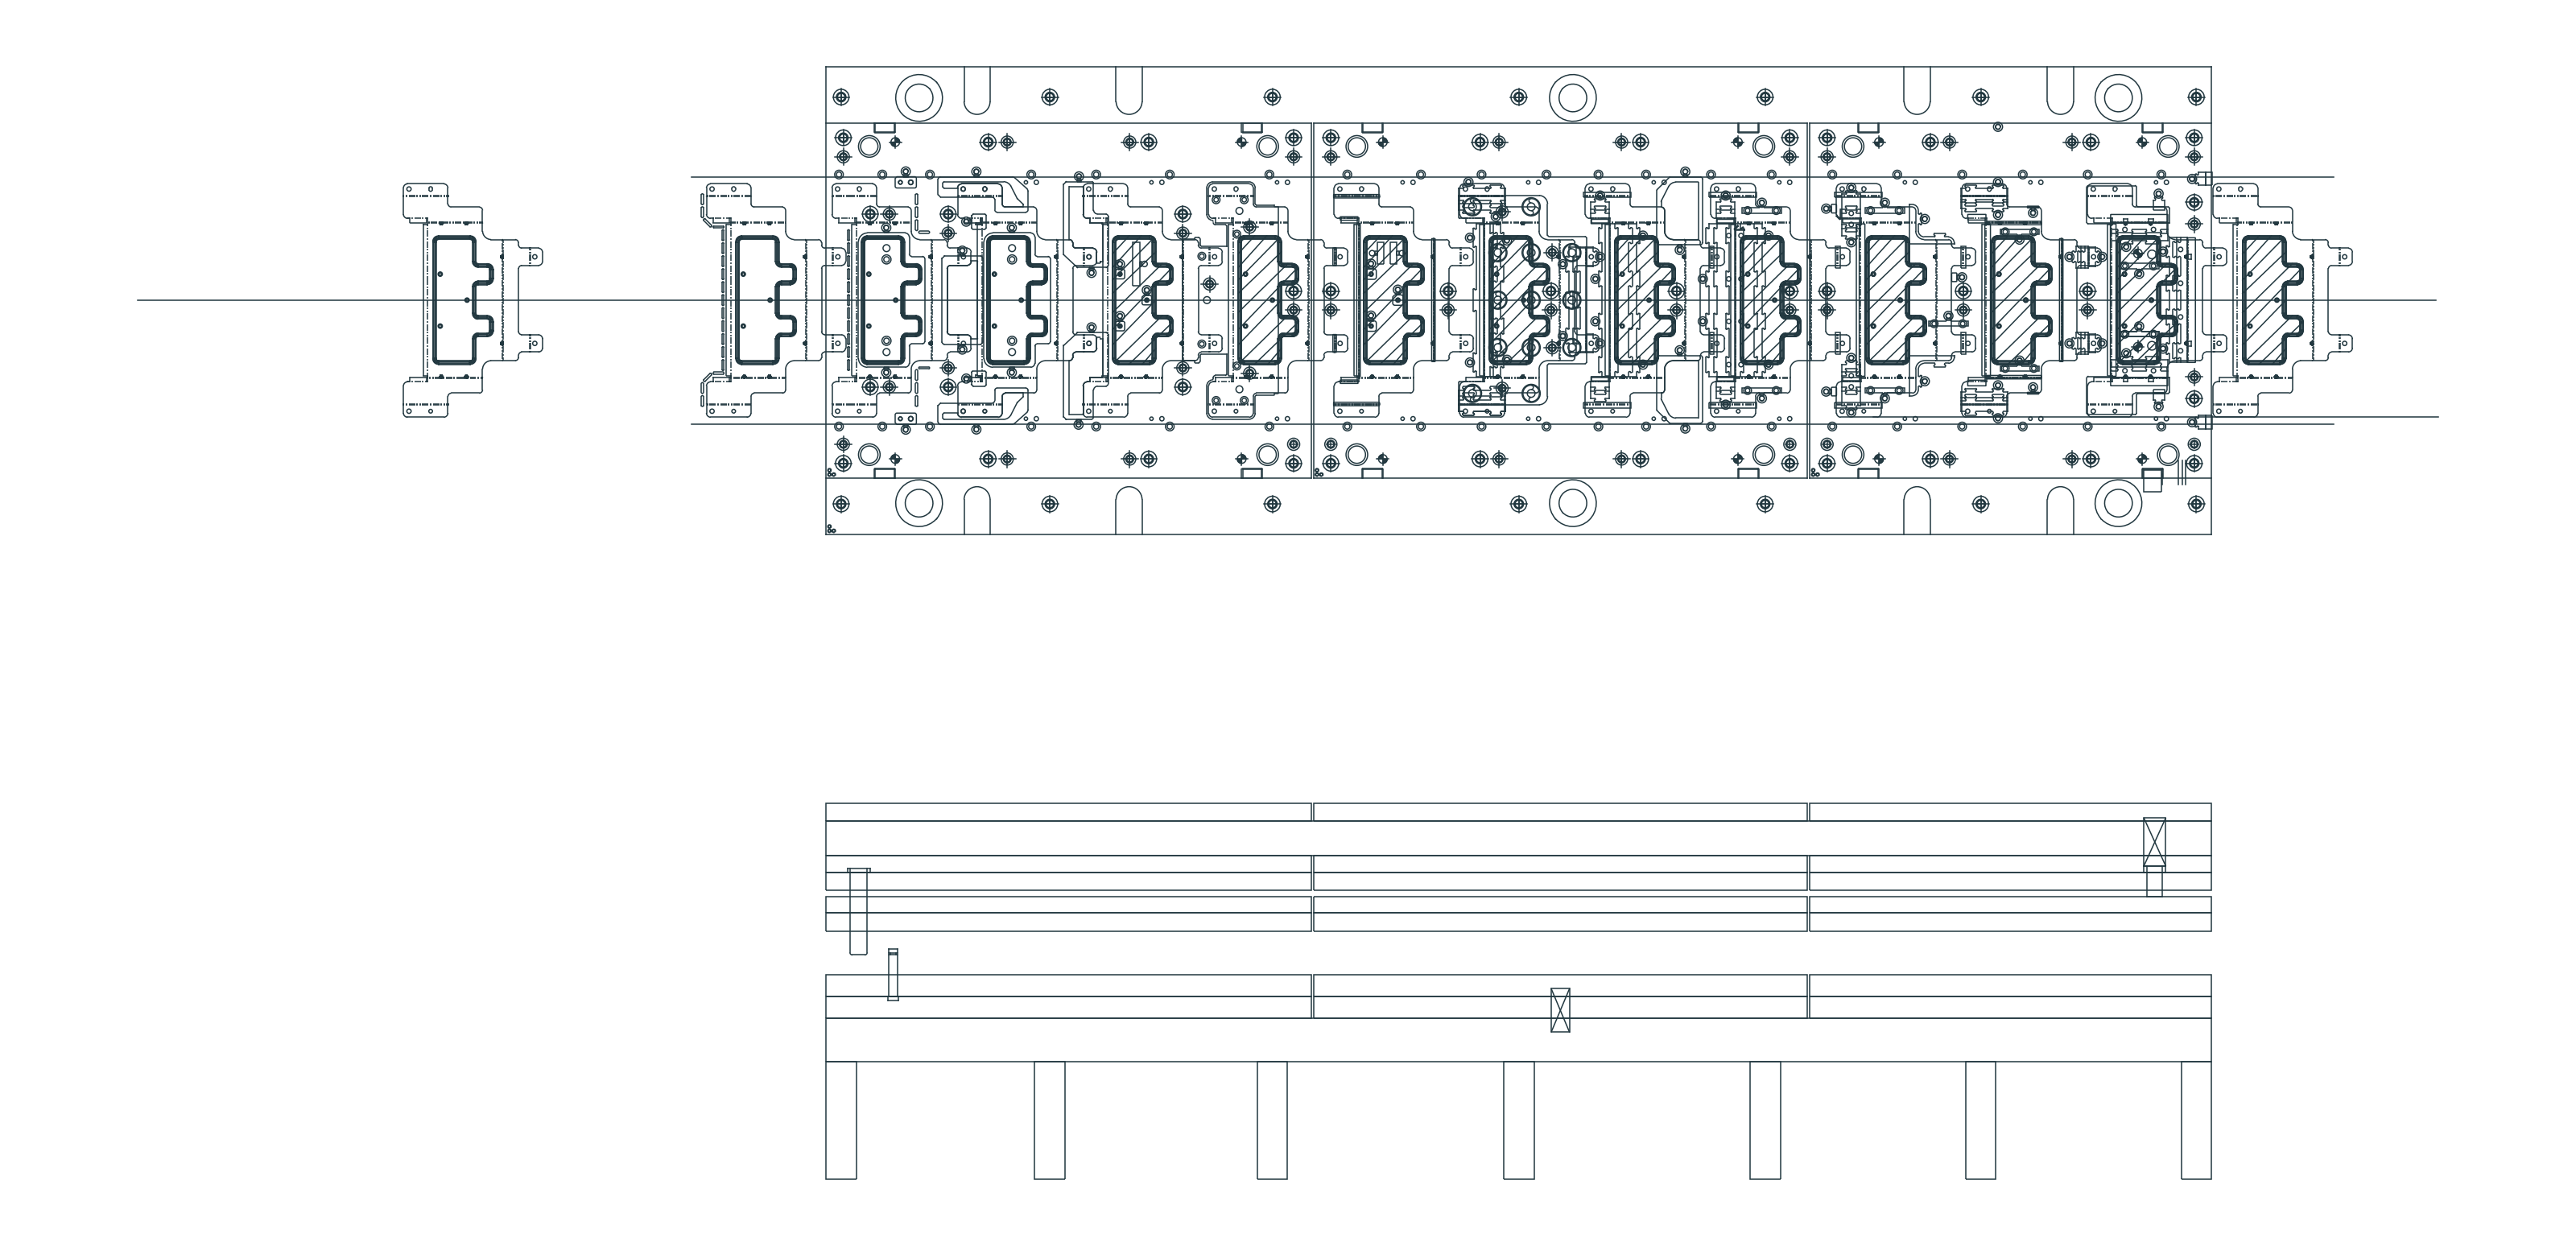
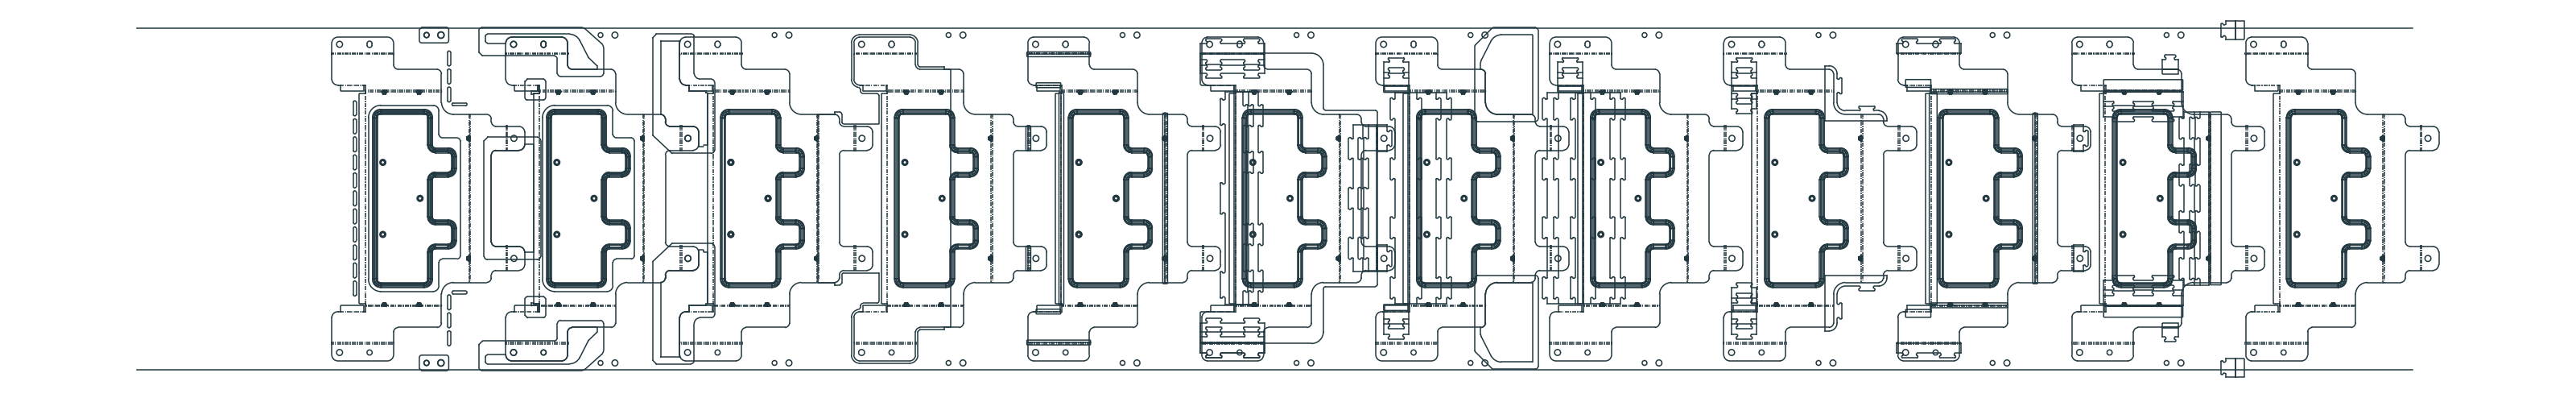
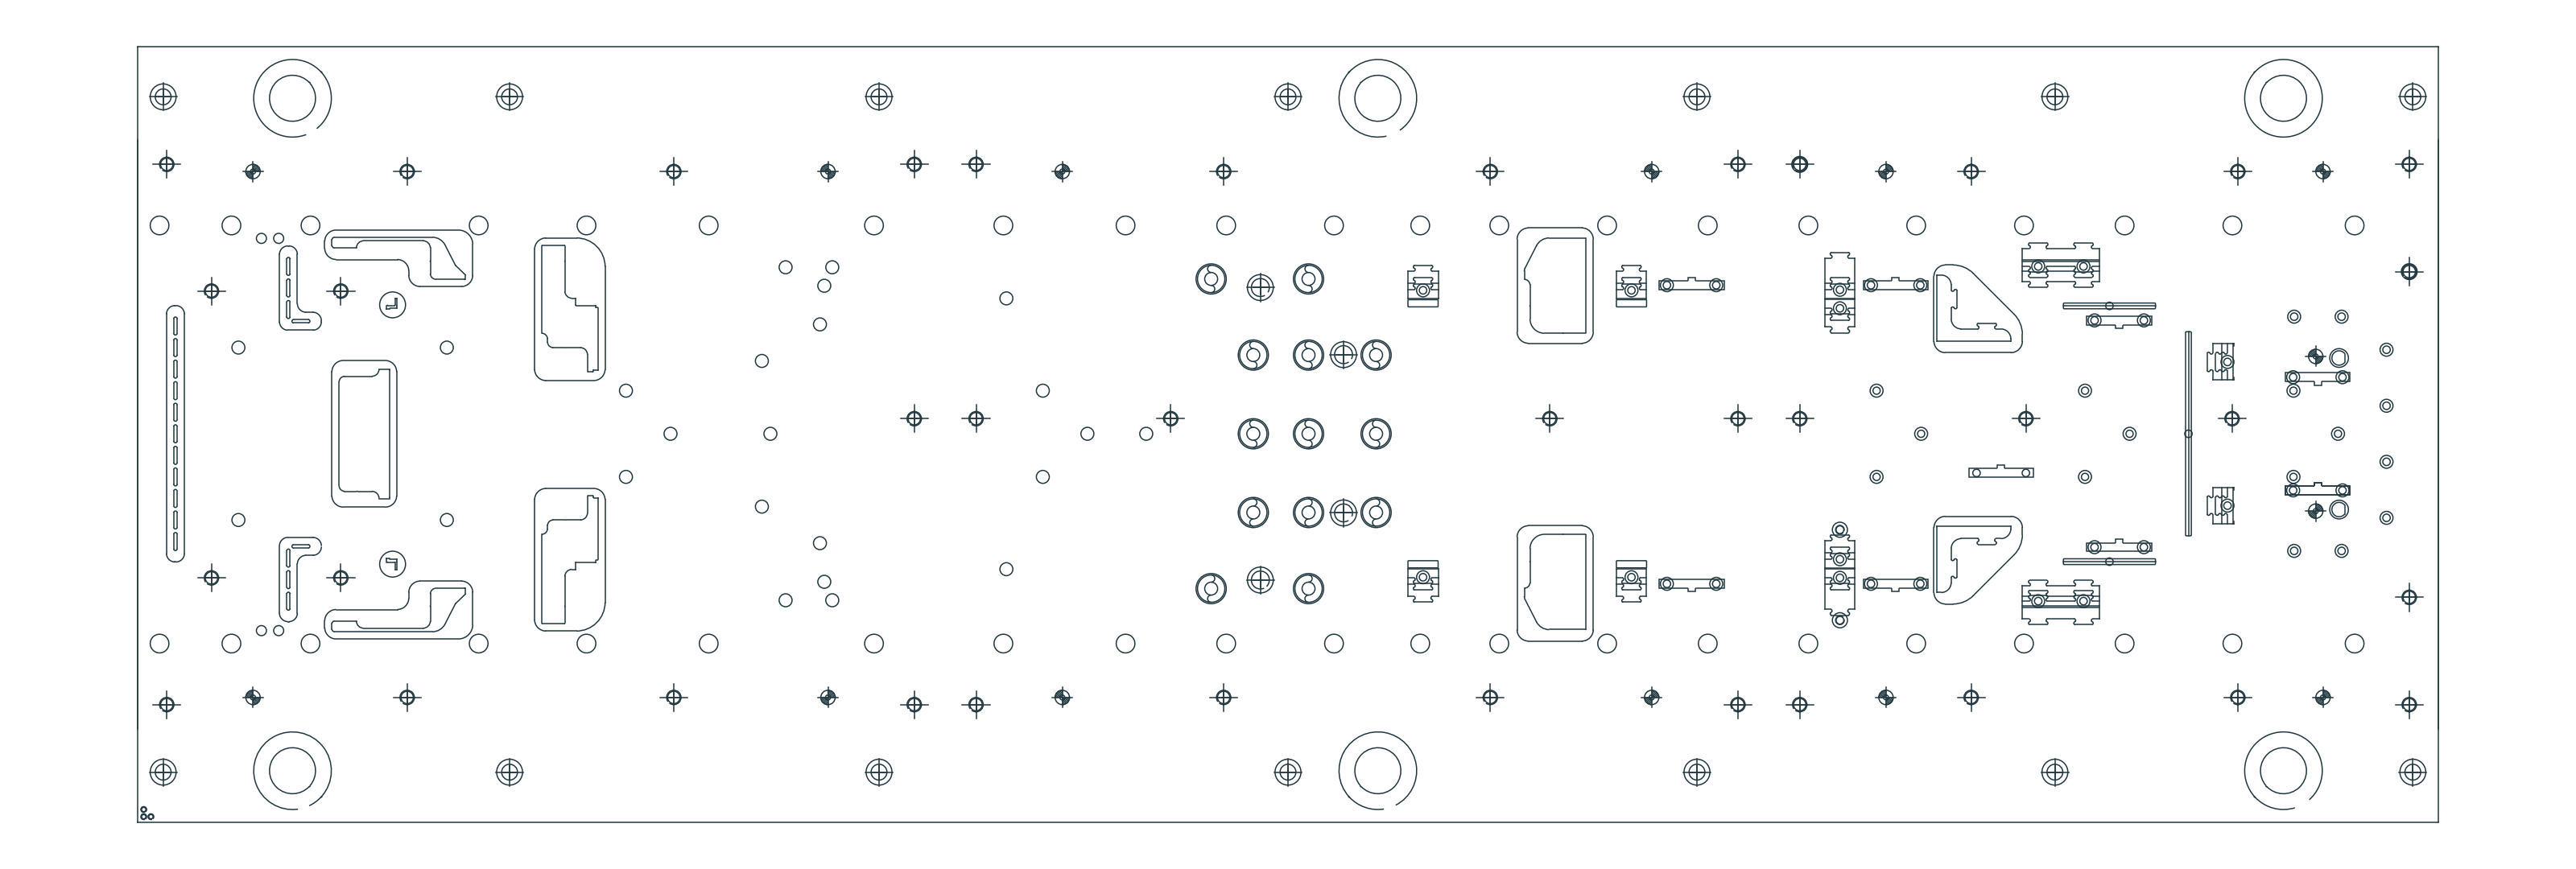
These previews show the die structure. Dimensions and manufacturing requirements are subject to the confirmed drawings.
Provide the part and tooling requirements together
A tooling quotation depends on the part, the expected use of the die and the validation work. Specify whether the die supports part production here or requires a separately agreed handover.
- Part drawing, material, thickness, critical features and expected production quantity.
- Sample stages, inspection reports and any receiving-press requirements.
- Required schedule, ownership and the agreed scope of tool delivery and support.
Common buyer questions
Have a question about your part? Leave a message and a reply email.
When is stamping tooling required?
Tooling is usually required when a custom metal part needs repeatable production, formed features, tight fit or progressive stamping efficiency. The exact tool type depends on geometry and volume.
What happens during T0, T1 and T2 die trials?
Trial stages produce sample parts, measure dimensions, check burr and forming quality, then feed corrections back into the die until the part is ready for approval.
What affects stamping die cost and lead time?
Part geometry, material thickness, forming depth, tolerance, annual volume, cosmetic requirements and inspection level can all affect die complexity, cost and timing.
How are tooling ownership and maintenance defined?
Agree ownership, storage location, maintenance scope, repair approval and any tool handover in the project terms. A part quotation alone does not define independent die delivery or a tool-life guarantee.
Your question has been recorded
Thank you. We will reply to the email address you provided. You do not need to submit again.
Question ID:
Review tooling scope before ordering
Send the part revision, material, thickness, quantities and acceptance points. List the requested samples, reports, tool storage or handover terms for confirmation in the quote.